Hydraulic Repair Case Studies from Our Sharjah Workshop
Every case study below is a real job from our workshop in Sharjah Industrial Area 13, with the fault we found, what we did, and the test result. Hydraulic equipment operates under punishing pressures, abrasive environments, and relentless duty cycles across the UAE. When internal wear, rod scoring, or cavitation causes machinery downtime, component restoration delivers OEM-standard performance at a fraction of replacement cost and turnaround time. Explore documented engineering overhauls executed in our workshop.
Root-Cause Teardown
Dimensional & metallurgical inspection
Bench Pressure Tested
Up to 350 bar hydrostatic verification
Documented Outcomes
Traceable workshop quality control
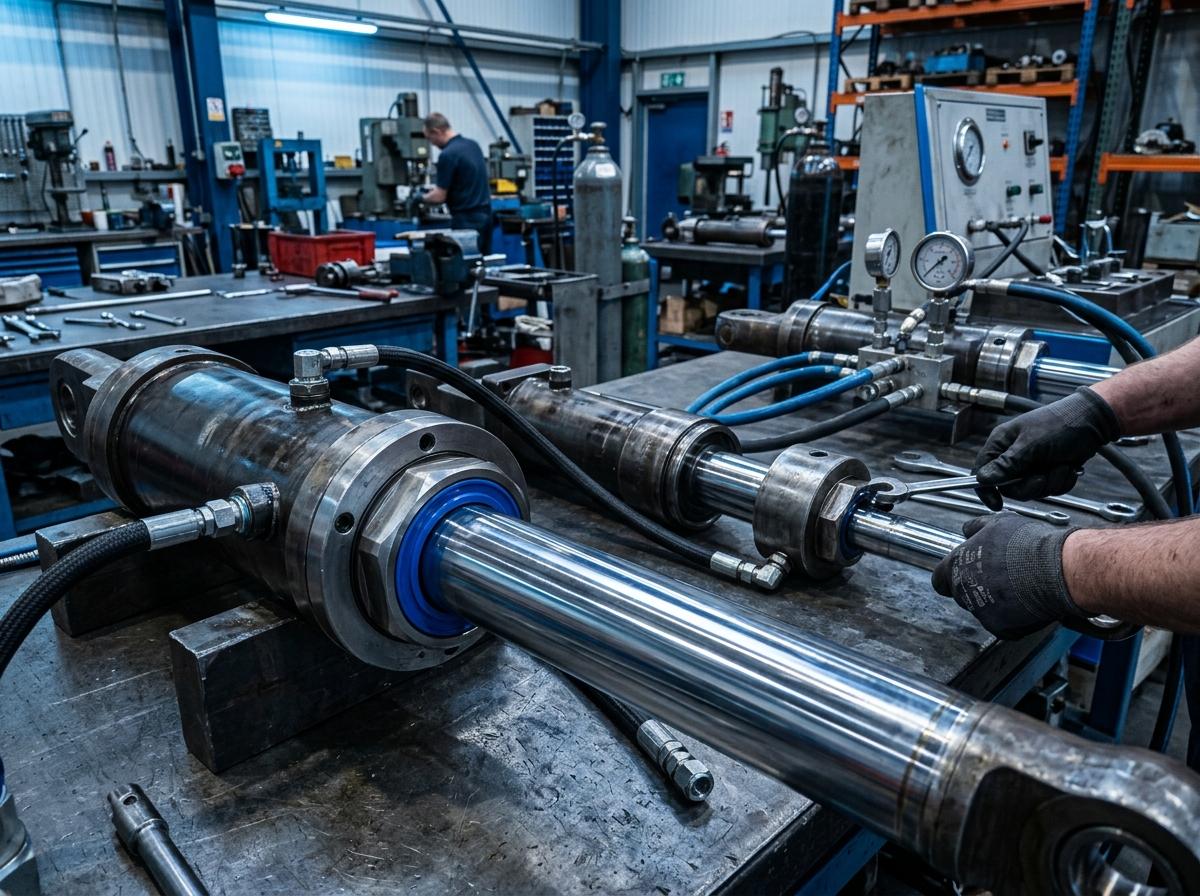
Boom Hydraulic Cylinder (280mm Bore)
ASAT Workshop, UAE
Large-Bore Excavator Boom Cylinder Overhaul
A 280 mm bore boom cylinder on an excavator working on a UAE infrastructure site was drifting under load and leaking at the gland. Sand past a damaged wiper had scored the rod and worn the piston seals. ASAT honed the barrel, restored the rod, fitted a new seal pack and held it at 350 bar for 30 minutes with no leakage.
The excavator suffered progressive lifting loss and external fluid weepage along the cylinder gland. Fine sand and abrasive grit had compromised the wiper seal, causing deep axial scoring along the chrome rod and internal fluid bypass across the piston seals.
The cylinder was unpinned, transferred to the workshop, and fully stripped on the teardown bench. The 280mm bore tube was checked for ovality and honed. The scored rod was polished and restored within OEM dimensional tolerance. A heavy-duty seal arrangement with reinforced guide rings was fitted prior to torque-controlled assembly.
The reassembled cylinder was mounted on the hydraulic test bench and cycled under 350-bar working pressure with zero internal bypass or gland leakage observed over a 30-minute hold cycle.
Documented Project Engineering Overhauls
Explore our technical capabilities across hydraulic cylinders, pumps, precision lathe machining, and valve assemblies.
Boom Hydraulic Cylinder (280mm Bore)
Large-Bore Excavator Boom Cylinder Overhaul
A 280 mm bore boom cylinder on an excavator working on a UAE infrastructure site was drifting under load and leaking at the gland. Sand past a damaged wiper had scored the rod and worn the piston seals. ASAT honed the barrel, restored the rod, fitted a new seal pack and held it at 350 bar for 30 minutes with no leakage.
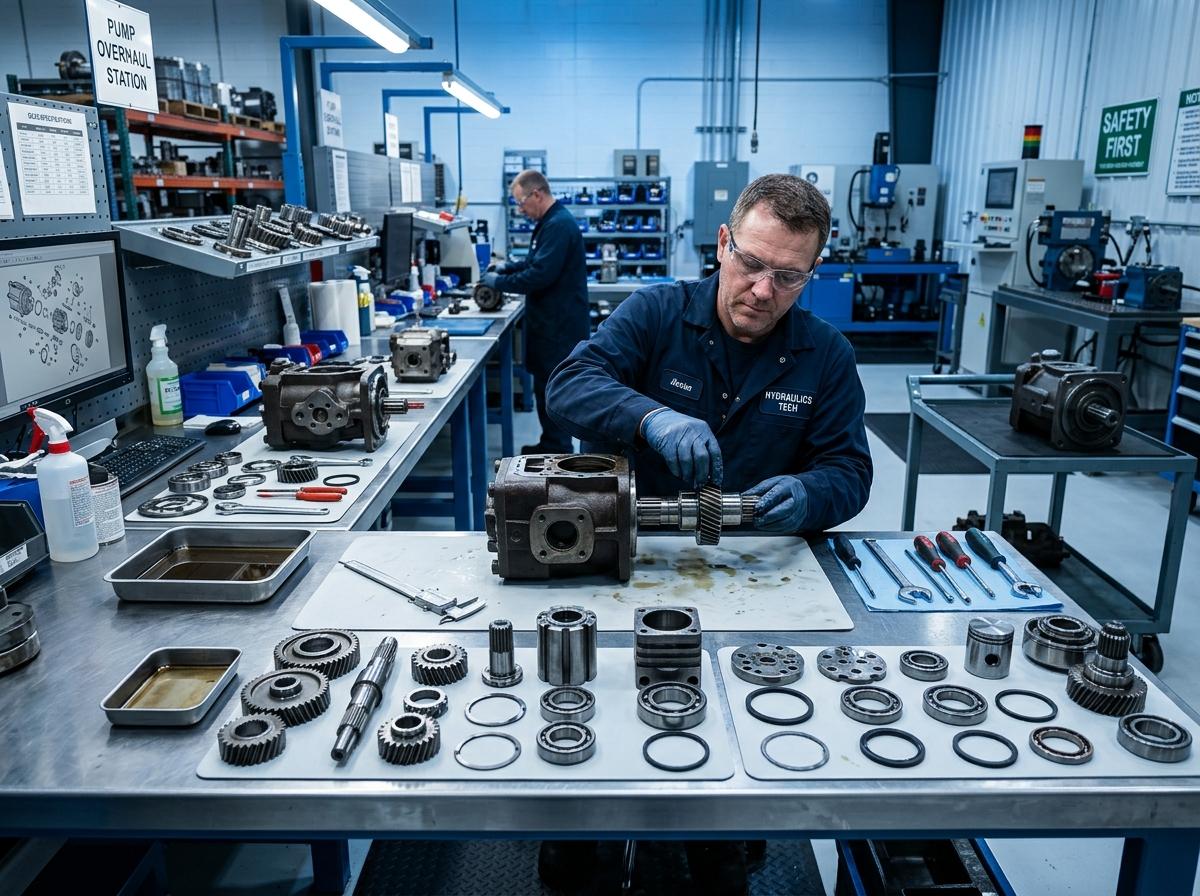
Axial Piston Main Hydraulic Pump
Variable Displacement Axial Piston Pump Overhaul
A 140 cc/rev variable displacement axial piston pump was whining, surging and slowing the machine's boom cycles. Teardown found cavitation pitting on the valve plate, worn slipper shoes and damaged cradle bearings. ASAT lapped the valve plate, renewed the rotating group, seals and bearings, then flow tested it from 500 to 1,800 RPM up to 320 bar.
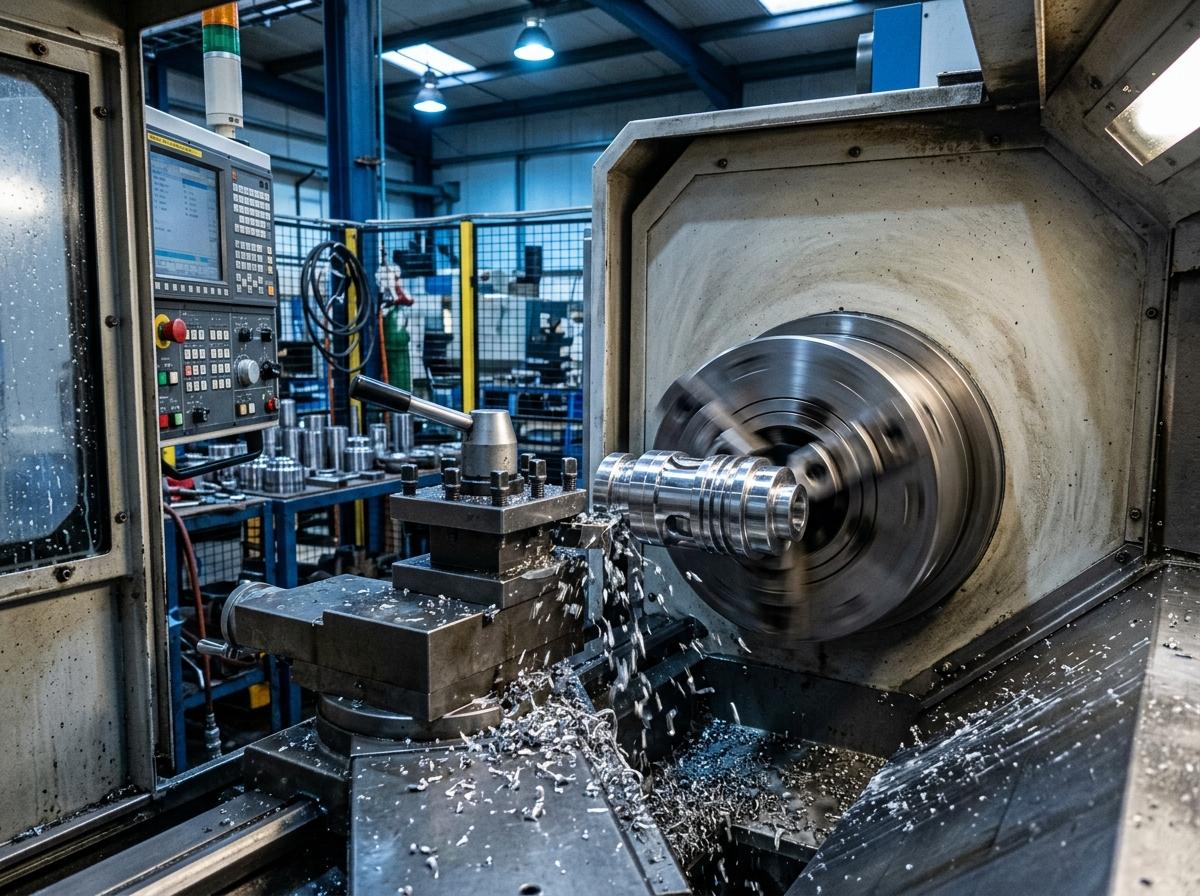
Custom Piston Rod & High-Load Bronze Bushings
Precision Machining of Custom Cylinder Rod & Bushings
An imported industrial press bent its 110 mm cylinder rod by 3.4 mm, and a factory rod would take 6 weeks to arrive. ASAT measured the damaged rod and mating parts, machined a new rod from 20MnV6 induction hardened chrome bar to ISO h7, made new aluminium bronze bushes and pressure tested the cylinder at 250 bar.
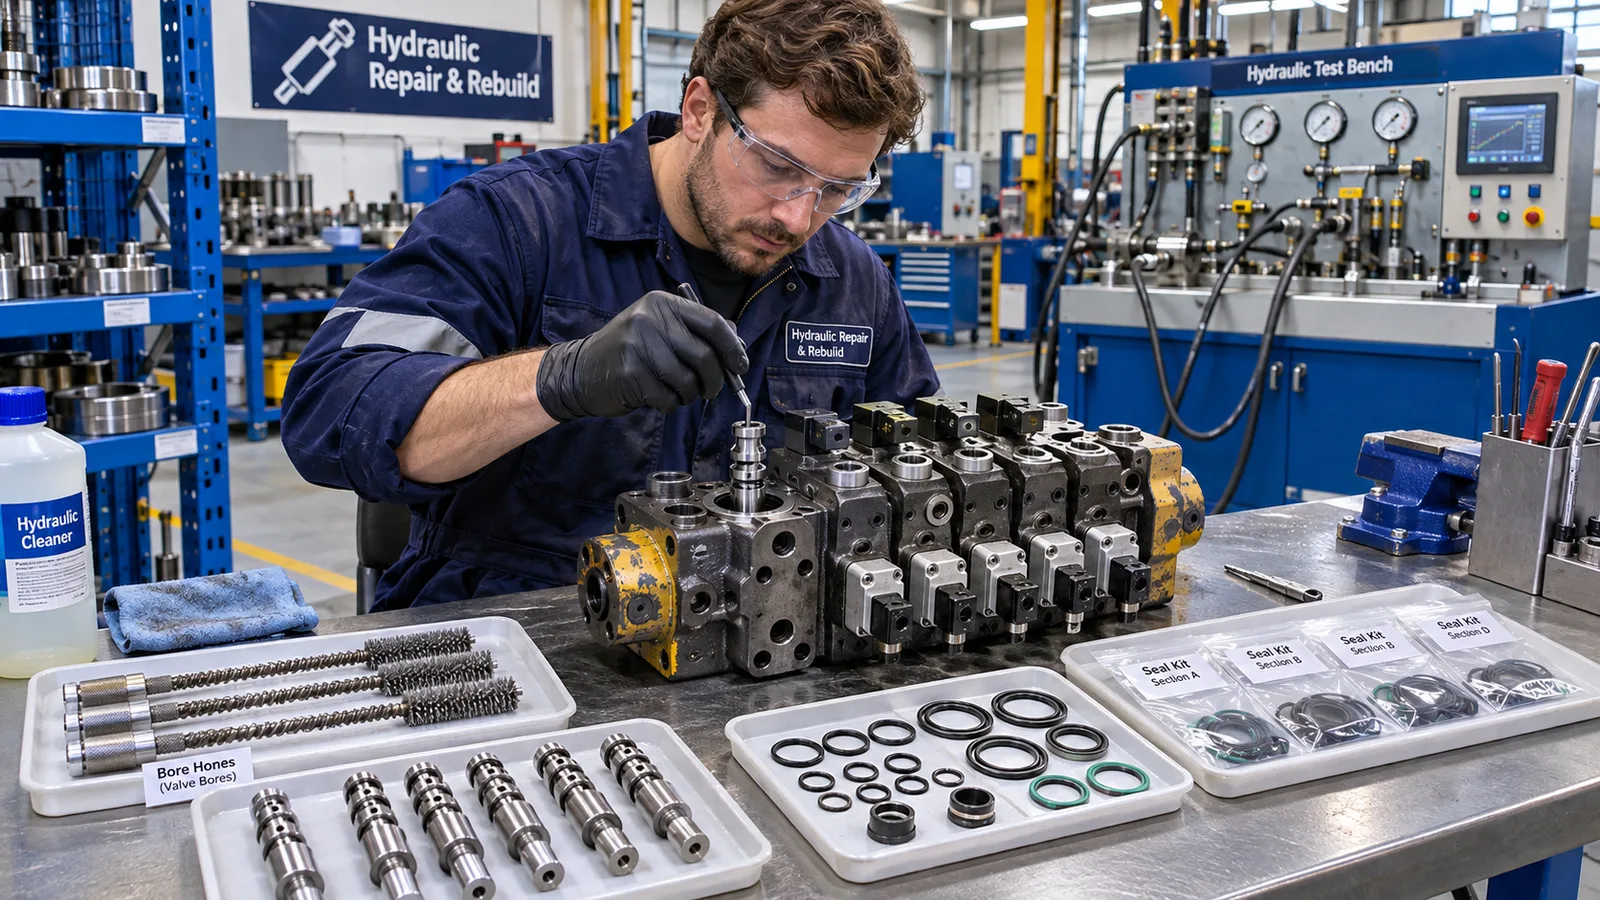
Multi-Spool Directional Control Valve Bank
Directional Control Valve Block Reconditioning & Spool Honing
A six section proportional valve from a mobile crane let the winch drift in neutral and had lost fine control. Varnish in the bores, scratched spools and a set relief spring had dropped relief pressure by 40 bar. ASAT honed the bores, lapped the spools, renewed every seal, reset the reliefs and tested the valve at 280 bar.
Facing an urgent hydraulic repair challenge?
Every equipment challenge requires methodical diagnostics and tailored engineering. Speak directly with our workshop engineers about your cylinder leakage, pump cavitation, or precision machining needs.
Technical Telephone
+971 58 958 4232Engineering Inquiries
info@asatuae.comService Area
Industrial Area 13, Near National Paints, Sharjah, UAE