Lathe Workshop and Precision Machining in Sharjah
ASAT's lathe workshop in Sharjah Industrial Area 13 turns, bores and threads hydraulic and heavy equipment parts to size. We make cylinder rods, glands, pistons, pins, shafts and bronze bushes from drawings, measurements or a damaged sample, so a broken part does not stop your machine for weeks.
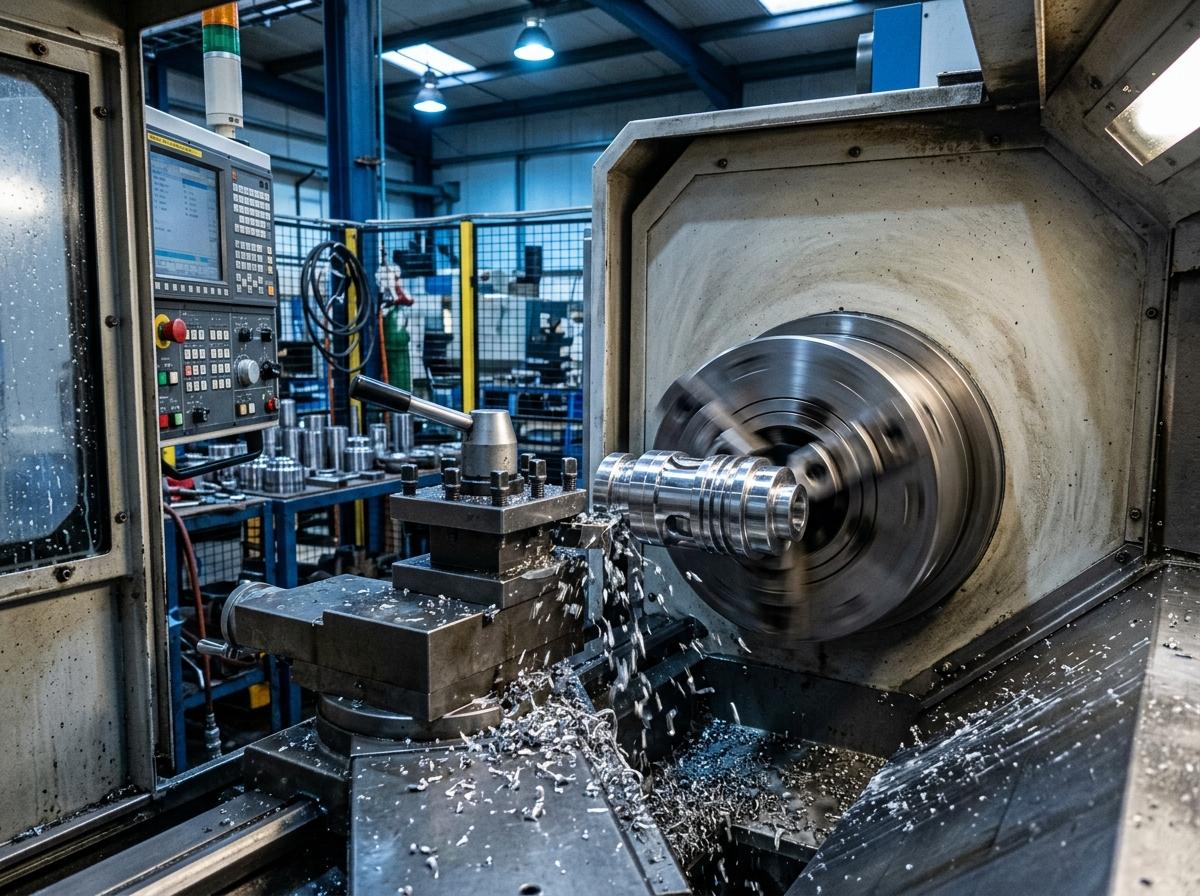
In-house lathe turning, boring & fabrication of custom hydraulic parts
A responsive hydraulic overhaul service depends on robust in-house machining capabilities. ASAT maintains industrial manual and precision lathes to turn, bore, thread, and finish components to exact engineering tolerances. We machine custom cylinder rods, glands, pistons, pins, and bronze bushings when original components are damaged or require immediate fabrication.
- Dedicated in-house industrial lathe turning and horizontal boring
- Custom fabrication for obsolete, non-standard, or long-lead hydraulic parts
- Strict micro-inch surface finish control for critical seal housings
How we machine a part
- 1.Engineering Measurement: Micrometer and caliper measurement of existing components or sample dimensions.
- 2.Material Selection: Selecting industrial-grade induction-hardened chrome bar, EN8, EN19, or phosphor bronze alloys.
- 3.Turning, Boring & Threading: Precision machining of seal grooves, thread pitches, and bore diameters to tight tolerances.
- 4.Surface Finishing: Polishing and micro-finishing bearing and seal surfaces to ensure extended packing longevity.
- 5.Quality Verification: Dimensional and concentricity verification before handover to workshop assembly teams.
Parts we machine
- Custom hydraulic cylinder rods & tie-rods
- Piston heads, rod glands & cylinder end caps
- Heavy equipment pivot pins & hardened steel bushes
- Hydraulic flanges, threaded adaptors & port manifolds
- Phosphor bronze and composite wear rings
- Shafts, keyways, splines and threads
Machining capacity
| Capability | Detail |
|---|---|
| Threading | Metric and imperial, single point |
| Typical tolerance | ISO h7 on rods and pins |
| Surface finish on seal faces | Ra 0.2 µm or better |
Making a part from a damaged sample
When there is no drawing, we measure the damaged part and the parts it fits into, then machine and trial fit the new one before final assembly. This is how we replace obsolete or slow to import parts on older machines.
Turnaround
Precision lathe machining: same day drawing review, 2–5 days turnaround, dimensional check to engineering tolerance.
Recent machining job
An imported industrial press bent its 110 mm cylinder rod by 3.4 mm, and a factory replacement had a 6 week import lead time. We reverse engineered the rod, turned a new one from induction hardened chrome bar to ISO h7, machined matching aluminium bronze bushes with grease grooves, kept runout under 0.02 mm and pressure tested the cylinder at 250 bar.
Lathe workshop FAQs
Can you make a part from a broken sample?
- Yes. We measure the sample and the mating parts, machine a replacement and trial fit it.
What tolerances can you hold?
- ISO h7 on rods and pins, with seal surfaces finished to Ra 0.2 µm or better.
How long does a machining job take?
- Usually 2 to 5 days after the drawing or sample is reviewed, which happens the same day.
Do you repair shafts?
- Yes. We turn new shafts and recut keyways, splines and threads.
Where is your lathe workshop?
- Industrial Area 13, near National Paints, Sharjah. Open 24 hours.
Start with a quote
Send the machine details. We quote after inspection, before any work starts. Open 24 hours.