Excavator Boom Cylinder Repair: 280 mm Bore, Held at 350 bar
A 280 mm bore boom cylinder on an excavator working on a UAE infrastructure site was drifting under load and leaking at the gland. Sand past a damaged wiper had scored the rod and worn the piston seals. ASAT honed the barrel, restored the rod, fitted a new seal pack and held it at 350 bar for 30 minutes with no leakage.
01. Project Overview
Operational Context & Requirement
A heavy-duty earthmoving excavator operating on a UAE infrastructure site developed severe lifting degradation and hydraulic fluid leakage around the main boom cylinder. ASAT Hydraulic Repairing was engaged to perform a comprehensive workshop teardown, root-cause diagnosis, precision refurbishment, and pressure testing prior to machine recommissioning.
02. Equipment & Component
Component Classification & Technical Parameters
Equipment Class
Heavy Earthmoving Excavator
Component Inspected
Boom Hydraulic Cylinder (280mm Bore)
- Cylinder Bore
- 280 mm
- Rod Diameter
- 160 mm
- Stroke Length
- 1,850 mm
- Test Pressure
- 350 bar (5,075 psi)
- Fluid Compatibility
- ISO VG 46 / 68 Hydraulic Oil
03. Initial Issue
Observed Fault & Symptoms
Equipment Failure Manifestation
The excavator suffered progressive lifting loss and external fluid weepage along the cylinder gland. Fine sand and abrasive grit had compromised the wiper seal, causing deep axial scoring along the chrome rod and internal fluid bypass across the piston seals.
Under standard payload conditions, the excavator boom drifted down gradually during operation, accompanied by visible hydraulic fluid leakage past the cylinder head gland. The hydraulic system experienced temperature elevation due to continuous internal oil bypass past the piston seals.
04. Inspection & Diagnosis
Teardown Findings & Root Cause Analysis
Visual and ultrasonic inspection of the cylinder barrel identified 0.12mm localized barrel wear near mid-stroke, within honing limits.
Surface profiling of the chrome-plated piston rod revealed multiple axial score lines exceeding 0.04mm depth caused by abrasive particle ingress past a degraded rod wiper.
The piston polyurethane seal assembly exhibited severe thermal hardening, extrusion damage, and lip breakdown.
End-cap threads and eye-bushings were dimensionally checked for concentricity and fatigue cracks.
05. Repair Methodology
Engineering Overhaul & Precision Machining Work
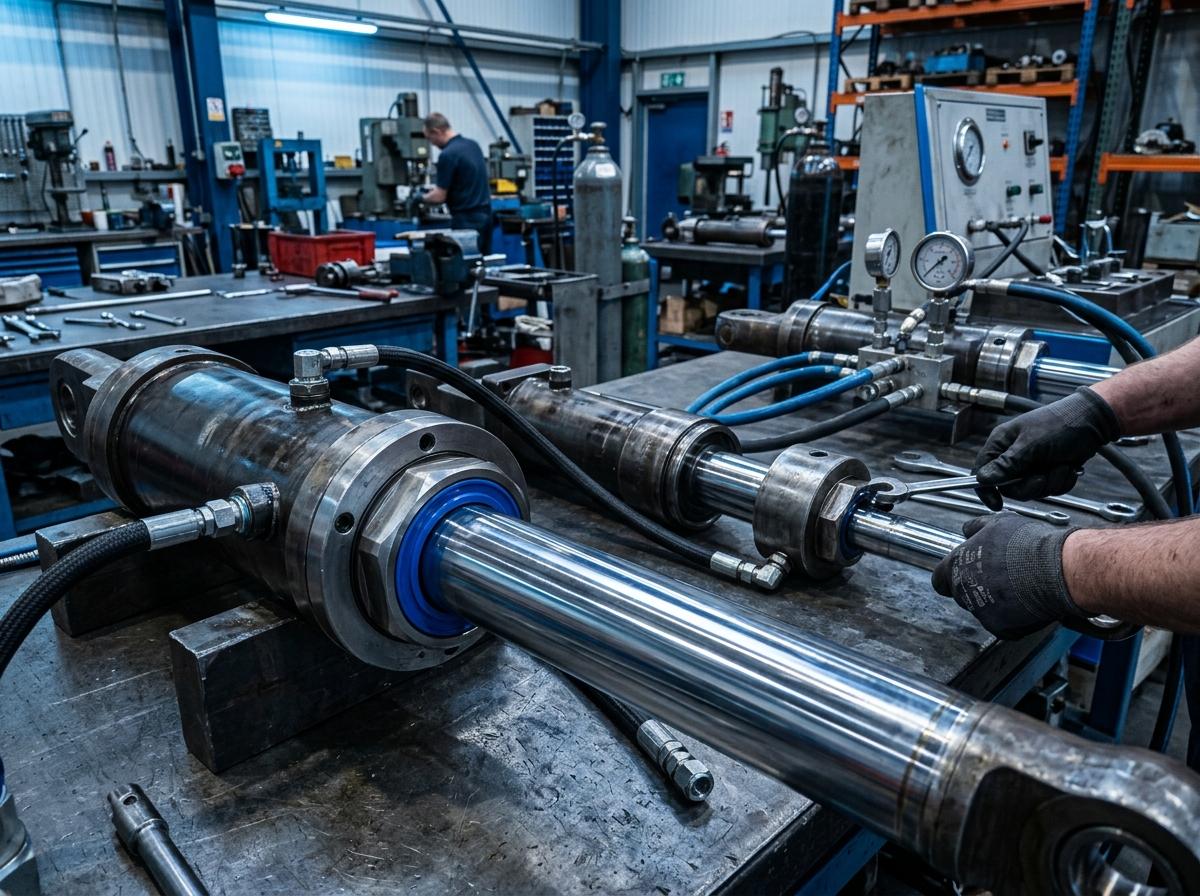
The cylinder was unpinned, transferred to the workshop, and fully stripped on the teardown bench. The 280mm bore tube was checked for ovality and honed. The scored rod was polished and restored within OEM dimensional tolerance. A heavy-duty seal arrangement with reinforced guide rings was fitted prior to torque-controlled assembly.
Detailed Work Execution Scope
- Cylinder barrel honing and micrometer dimensional check
- Piston rod inspection, de-burring, and hard-chrome finishing
- Installation of OEM-spec polyurethane high-pressure seal package
- Full static and dynamic pressure test at 350 bar
06. Testing & Verification
Hydrostatic Pressure Benchmark & Quality Assurance
- Static pressure hold test conducted on the ASAT hydraulic test rig at 350 bar for 30 minutes.
- Zero measurable fluid drop across the piston seals during dual-chamber pressure monitoring.
- Full stroke cycling at varied flow rates to confirm smooth gland wiper operation and absence of stick-slip friction.
- Final visual inspection, port capping, and high-durability industrial protective priming.
The reassembled cylinder was mounted on the hydraulic test bench and cycled under 350-bar working pressure with zero internal bypass or gland leakage observed over a 30-minute hold cycle.
07. Final Outcome
Delivered Performance & Operational Return
A 280 mm bore boom cylinder on an excavator working on a UAE infrastructure site was drifting under load and leaking at the gland. Sand past a damaged wiper had scored the rod and worn the piston seals. ASAT honed the barrel, restored the rod, fitted a new seal pack and held it at 350 bar for 30 minutes with no leakage.